


Home

Products
Products
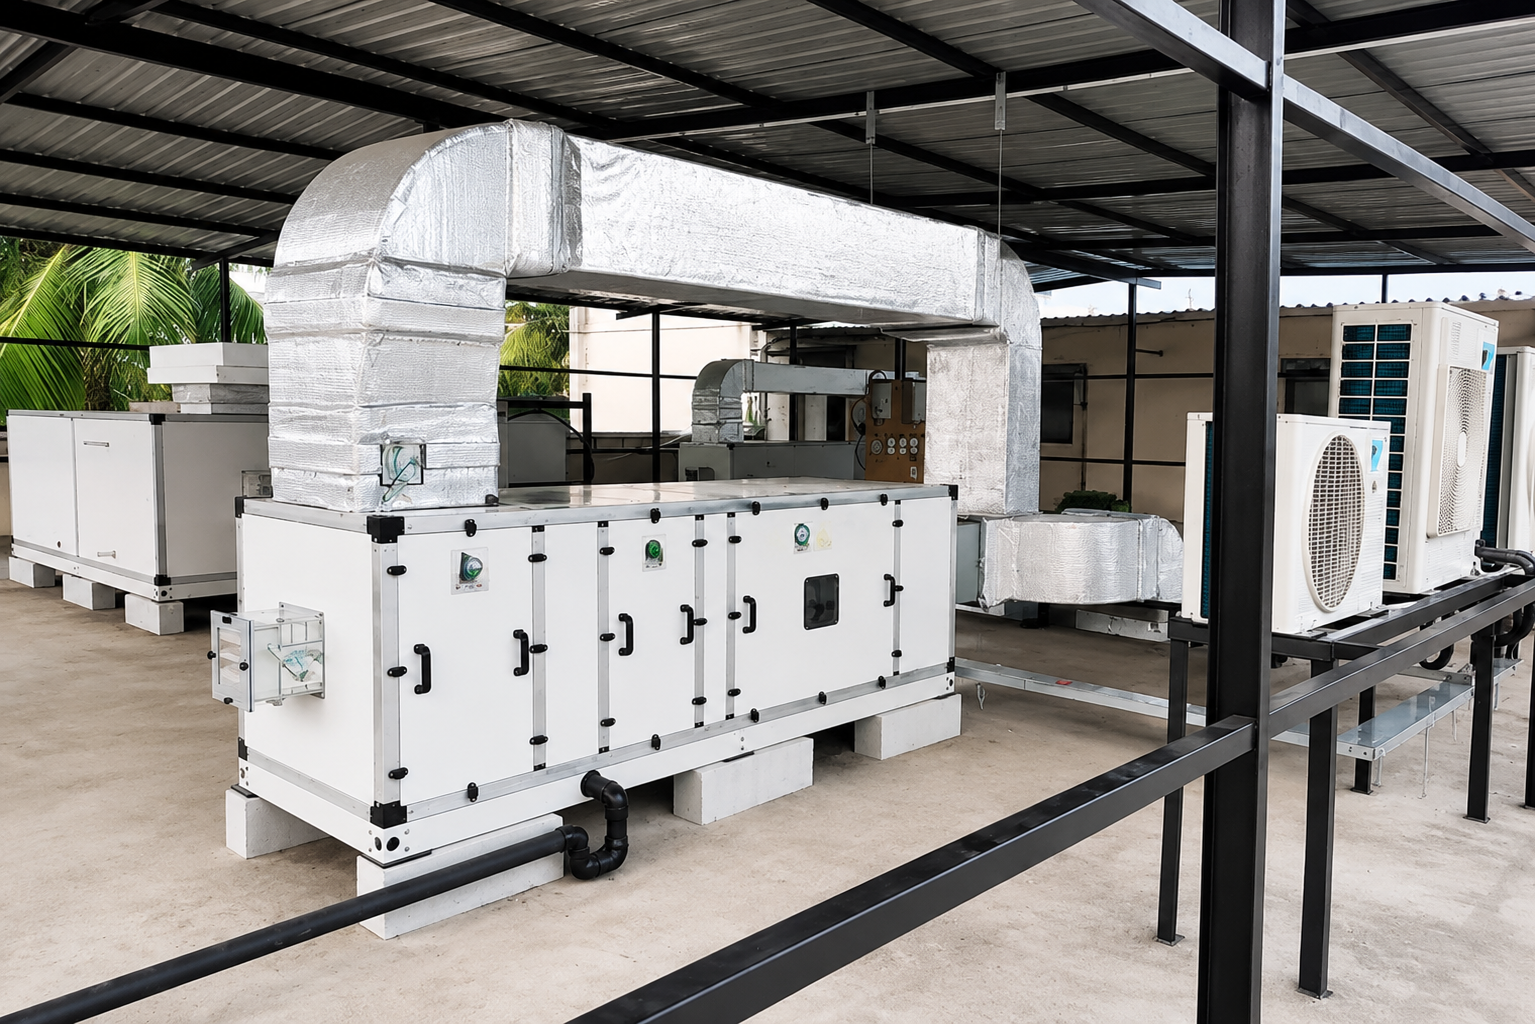
Air Handling Units
Centralized Air Management for Clean Environments
Custom-engineered AHUs for cleanrooms, pharmaceutical facilities, hospitals and industrial environments, providing controlled filtration, airflow, temperature and humidity.
Key Features
- Pre, Fine & HEPA/ULPA filtration
- Temperature & humidity control
- Custom airflow & pressure configurations
- Energy-efficient fan systems
- BMS integration options
- Hygienic construction


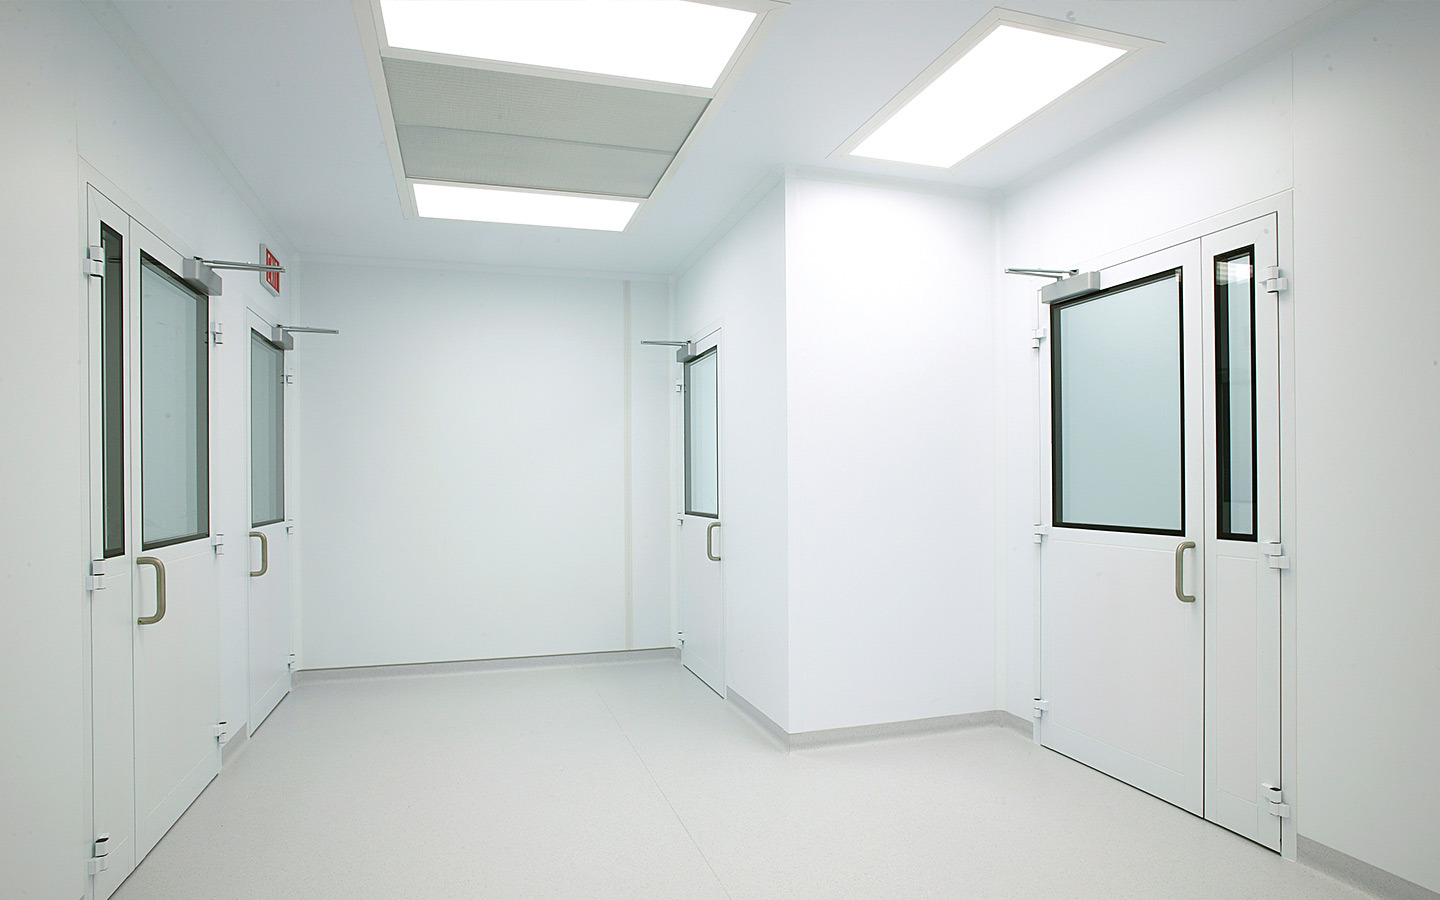
Modular Cleanroom Panels
Modular Cleanroom Panels
High-Performance Cleanroom Enclosures
Modular wall and ceiling systems engineered for hygienic, durable and controlled cleanroom environments.
Key Features
- PUF & Rockwool insulation
- SS, PPGI & HPL finishes
- Cam-lock & tongue-and-groove joints
- Easy-to-clean surfaces
- Fire-retardant options
- Custom dimensions
Applications
Pharmaceuticals | Electronics | Biotechnology | Food Processing | Healthcare | Diagnostics

.jpeg)
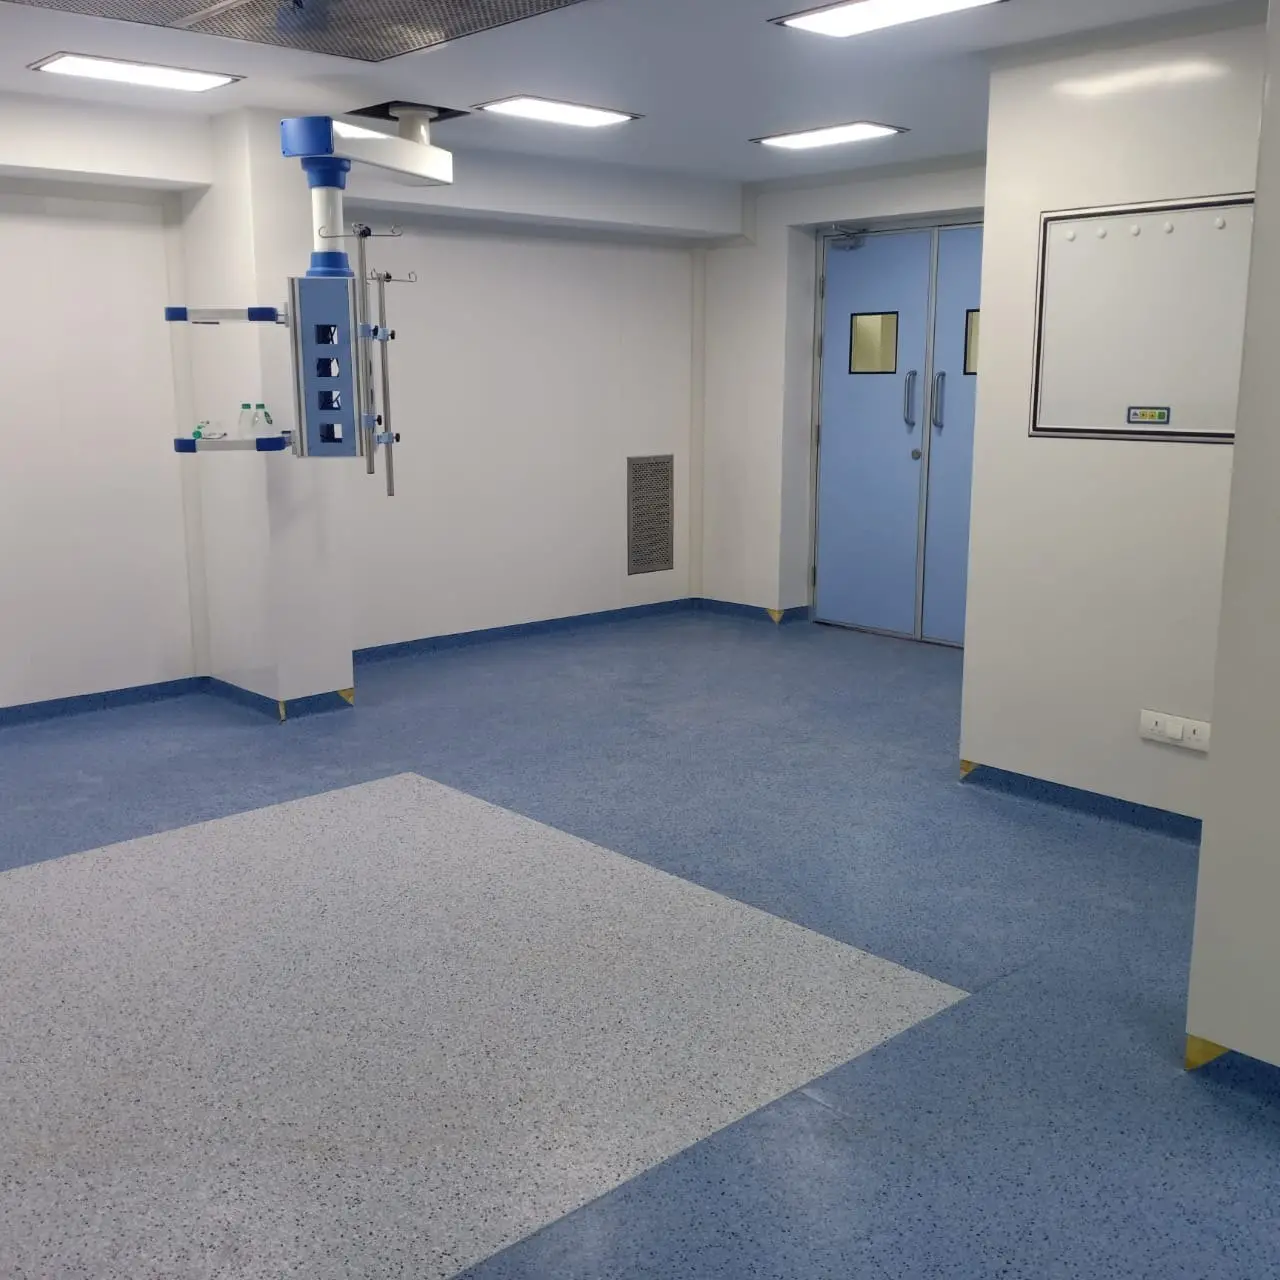
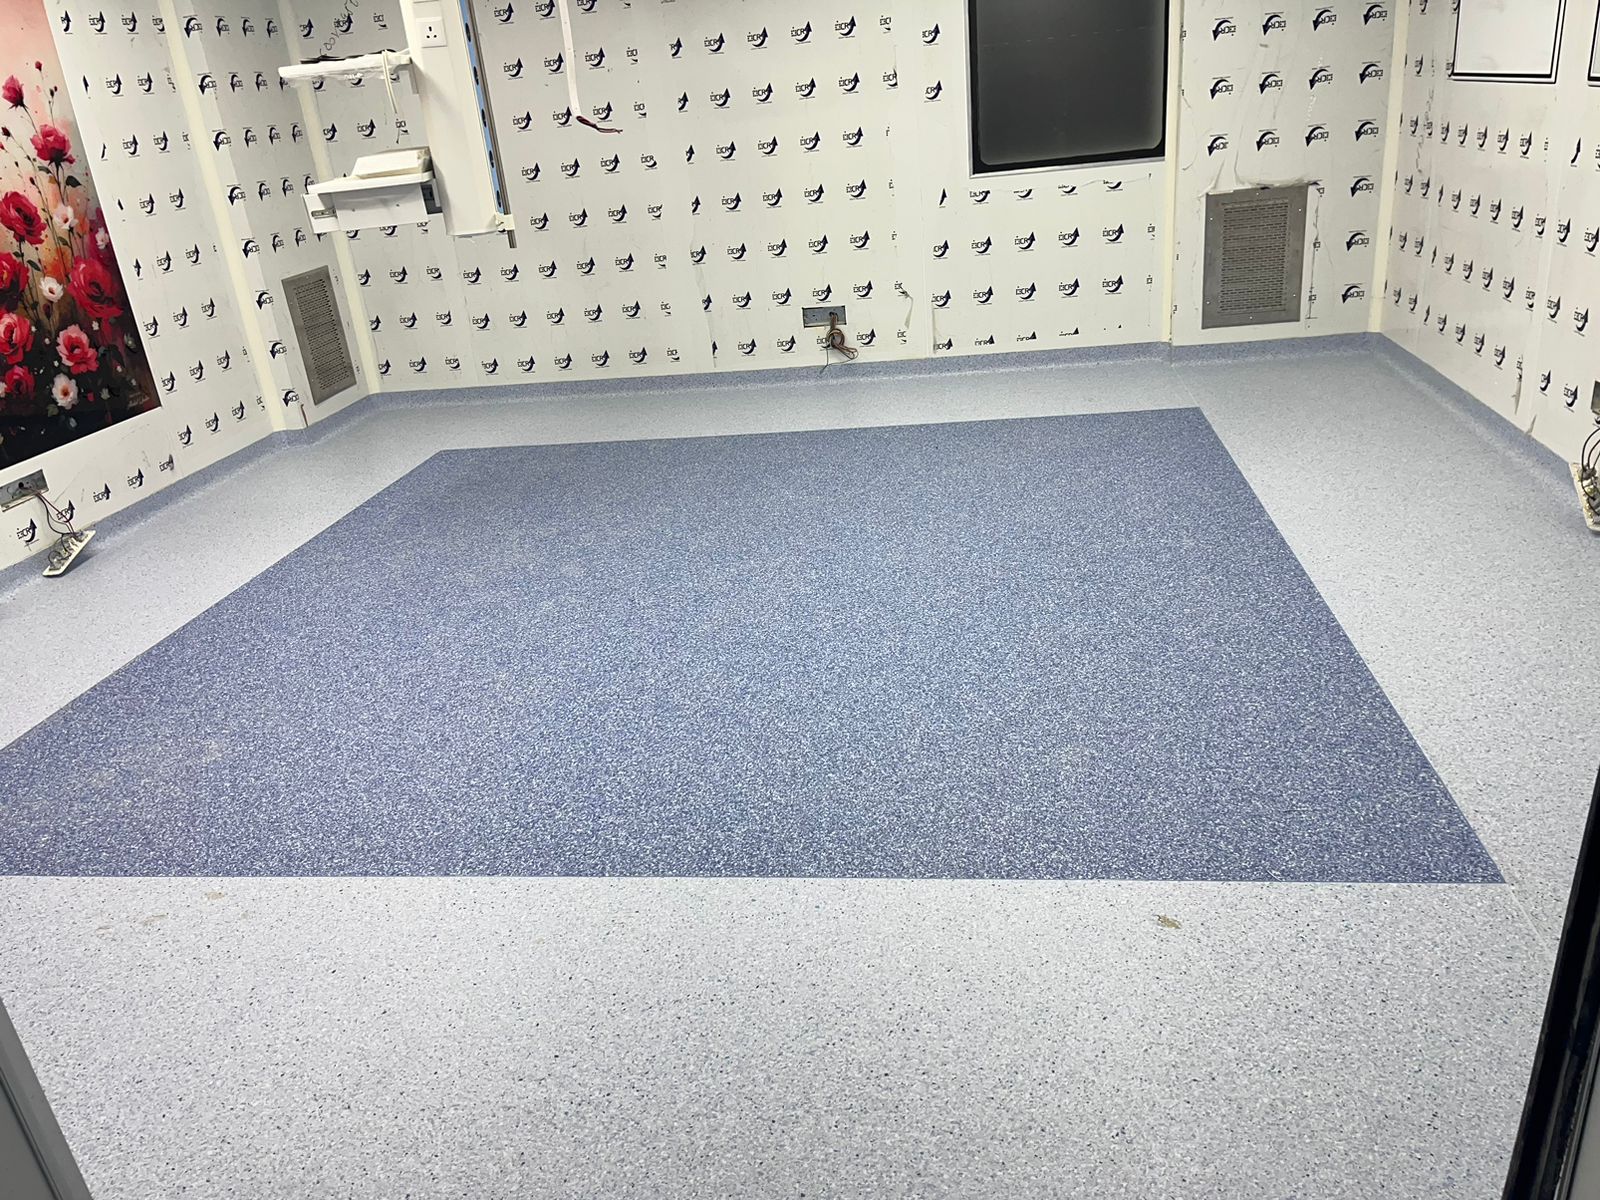
Flooring & Coving Solutions-
Seamless Hygienic Surfaces
Cleanroom flooring and coving solutions designed for durability, hygiene, chemical resistance and easy maintenance.
Solutions
- Epoxy Flooring — Seamless & chemical-resistant
- Vinyl Flooring — Hygienic & resilient
- Coving Systems — Smooth, easy-clean transitions
Key Features
- Seamless finishes
- Chemical-resistant options
- Slip-resistant options
- ESD / conductive options
- Custom coving profiles
.jpeg)
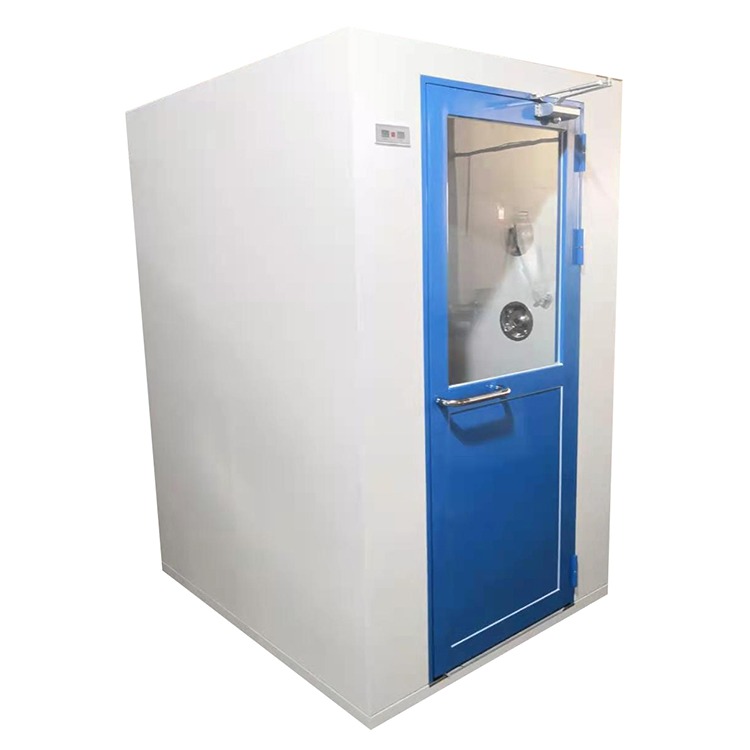
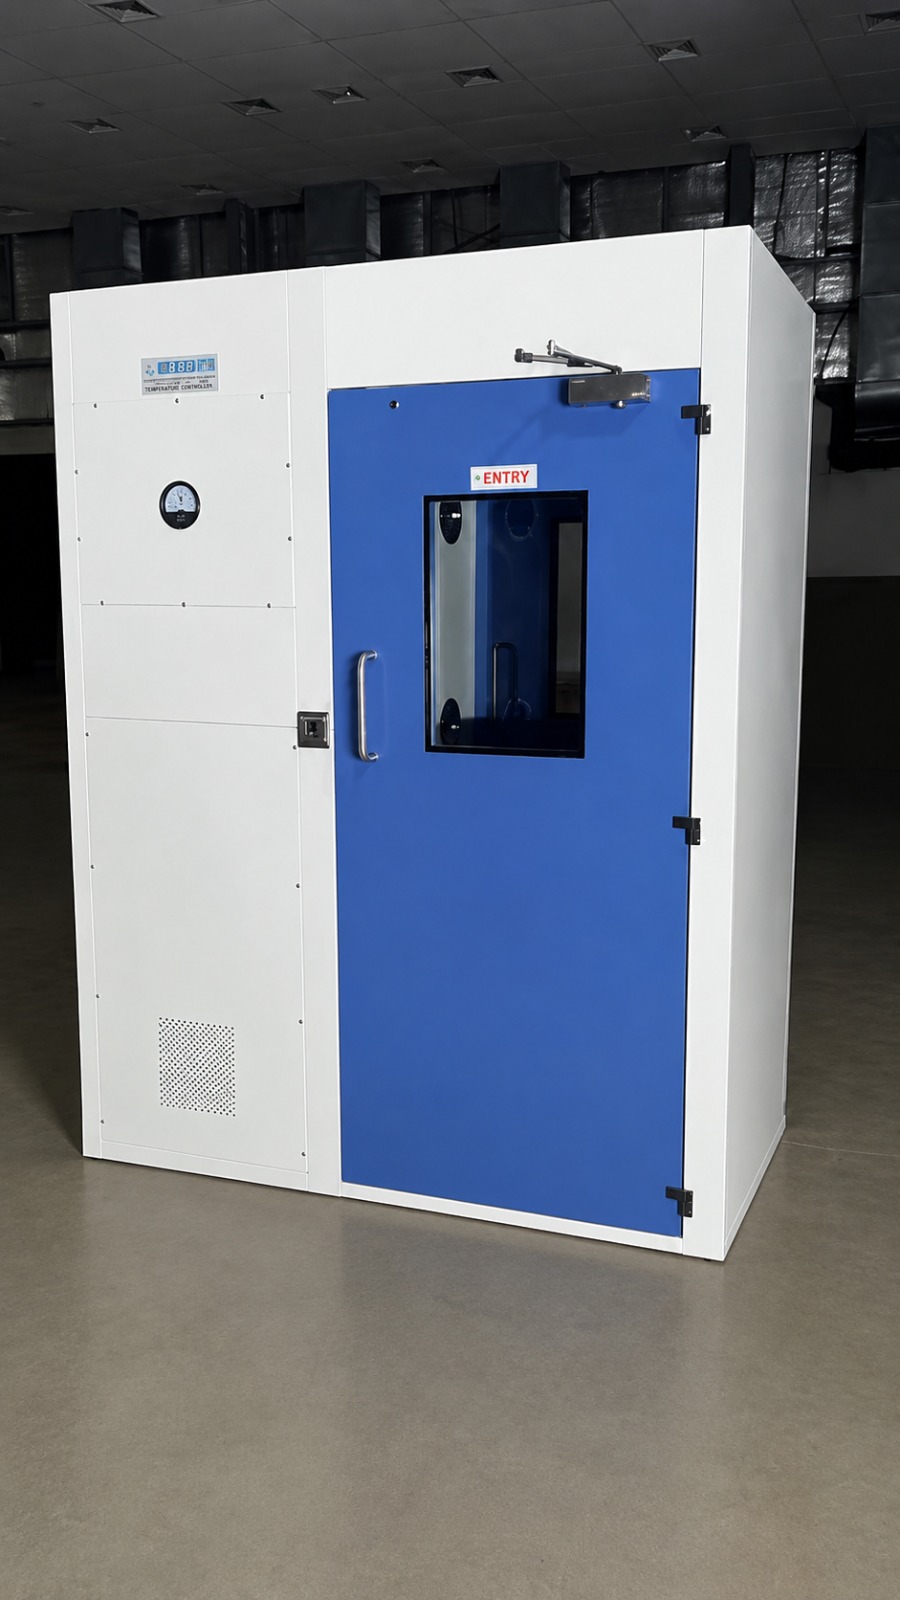
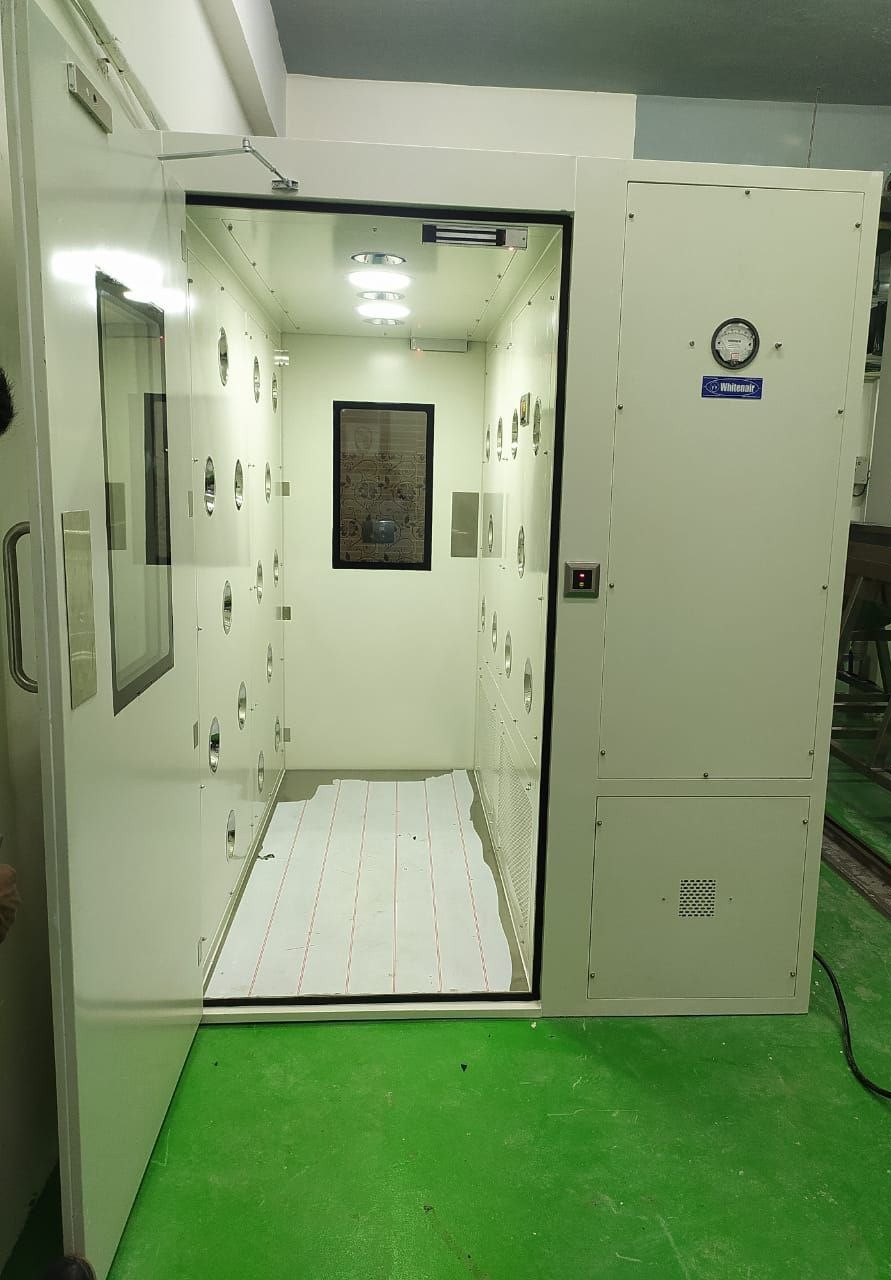
Air shower
Personnel & Material Contamination Control
At Advanced Cleanroom Solutions, we provide high-performance Air Showers engineered to decontaminate personnel, equipment, and materials before entry into critical controlled environments. These self-contained chambers utilize high-velocity, HEPA-filtered air jets to effectively dislodge and remove surface particles, significantly reducing the risk of contamination within cleanrooms.
✅ Key Features
- Robust Construction: Available in stainless steel or powder-coated finishes for durability and easy maintenance
- High-Velocity Air Jets: Delivers air at 20–25 m/s to ensure efficient particle removal
- HEPA/ULPA Filtration: Equipped with HEPA (99.99% @ 0.3μ) or optional ULPA filters for maximum air purity
- Intelligent Access Control: Automatic door interlocking system to prevent simultaneous door opening
- User-Friendly Interface: Operable via touchscreen or push-button control panel
- Flexible Configurations: Offered in single-side, double-side, L-type, and fully customizable layouts
Applications
• Pharmaceuticals
• Biotechnology
• Hospitals & Healthcare Clean Zones
• Electronics & Semiconductor Manufacturing
• Cleanroom and Controlled Manufacturing Environments
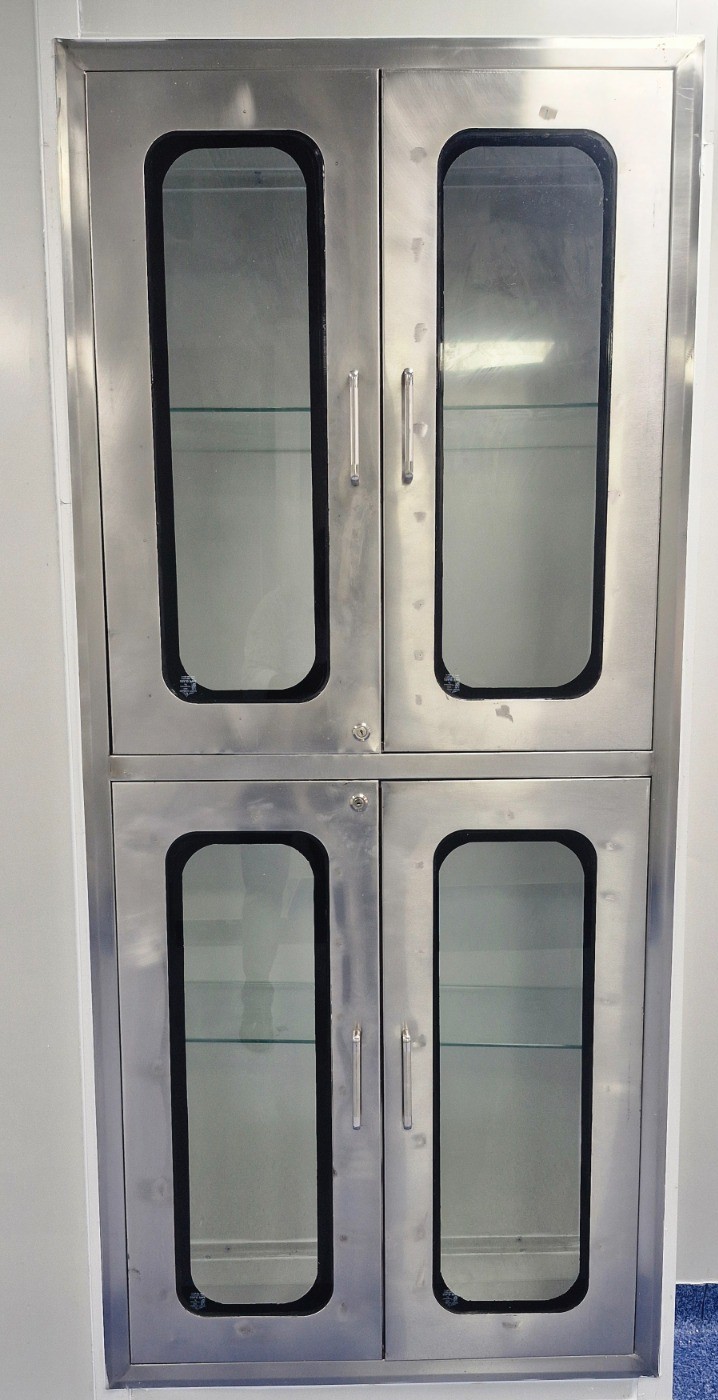
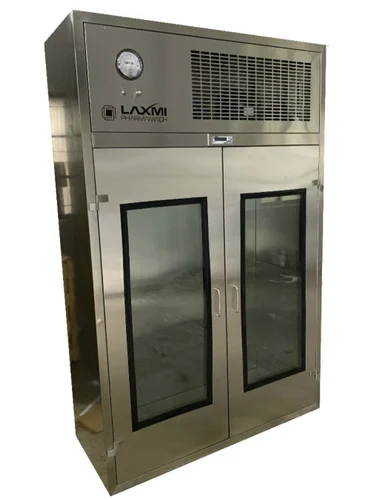
Sterile Garment Storage Cabinet
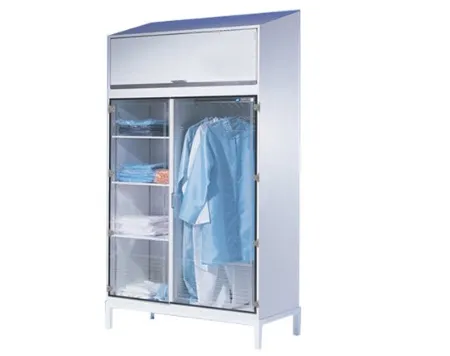
Sterile Garment Storage Cabinets
By Advanced Cleanroom Solutions
Advanced Cleanroom Solutions offers Sterile Garment Storage Cabinets specifically designed to store and protect cleanroom garments in a contamination-free environment. These cabinets play a crucial role in upholding cleanroom hygiene protocols, particularly in pharmaceutical, biotechnology, and healthcare settings.
✅ Key Features
- 304/316 Stainless Steel Construction: Ensures long-term durability, corrosion resistance, and compliance with cleanroom standards
- HEPA-Filtered Air Circulation
- UV Light Sterilization (Optional)
- Transparent Doors: Available with acrylic or tempered glass
- Flexible Storage Options: Equipped with adjustable shelves and hanger rods
- Installation Flexibility: Offered in both floor-mounted and wall-mounted
Applications :
Our sterile garment cabinets are essential in:
• Pharmaceutical Facilities
• Hospitals & Surgical Zones
• Biotechnology Laboratories
• Clean Manufacturing Units
Dynamic Pass Box (DPB)
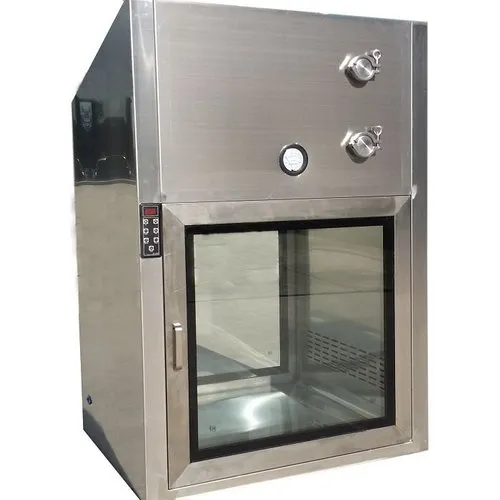
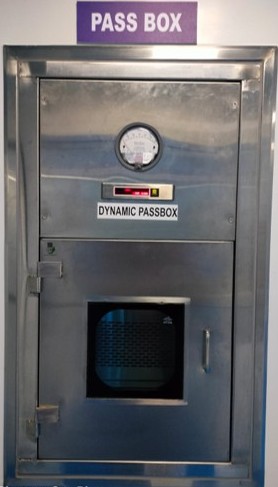
Dynamic Pass Box (DPB) for Controlled Material Transfer
The Dynamic Pass Box from Advanced Cleanroom Solutions is an essential equipment for the contamination-free transfer of materials between clean and non-clean areas. Engineered to maintain a sterile internal environment, the DPB minimizes the risk of cross-contamination with continuous air circulation and high-efficiency filtration—making it a critical component in cleanroom protocols.
✅ Key Features
- High-Efficiency Filtration HEPA/ULPA filters
- Interlocking Doors
- Built-in Blower Unit
- Stainless Steel Construction: Fabricated in SS 304/316 with cleanroom standards
- UV Sterilization (Optional): Integrated UV light for enhanced microbial control
- Internal Illumination: Bright and energy-efficient fluorescent or LED lighting for visibility during transfer
- Flexible Installation: Available in floor-mounted and wall-mounted configurations
Applications :
• Pharmaceuticals
• Biotechnology
• Diagnostic & Research Laboratories
• Electronics & Semiconductor Manufacturing
• Food & Beverage Processing
.webp)
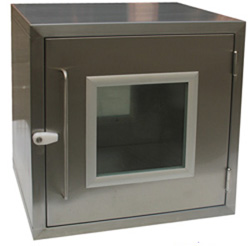
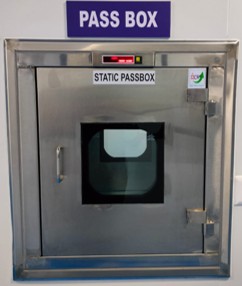
Static Pass Box (SPB)
Static Pass Box (SPB)
By Advanced Cleanroom Solutions
The Static Pass Box from Advanced Cleanroom Solutions is a reliable and space-efficient system designed for the safe transfer of non-sensitive materials between cleanrooms or between rooms of different cleanliness classifications—without disrupting the environmental integrity. Unlike dynamic pass boxes, SPBs operate without air circulation or filtration, making them ideal for low-risk zones where contamination control is still a priority.
✅ Key Features
- SS 304 / SS 316 options
- Mechanical / electromagnetic interlock
- Optional UV treatment
- Toughened-glass panels
- Easy-clean interiors
- Custom dimensions
Applications: Pharmaceutical | Hospitals & Cleanroom Wards | Healthcare | Biotechnology | Laboratories
.webp)
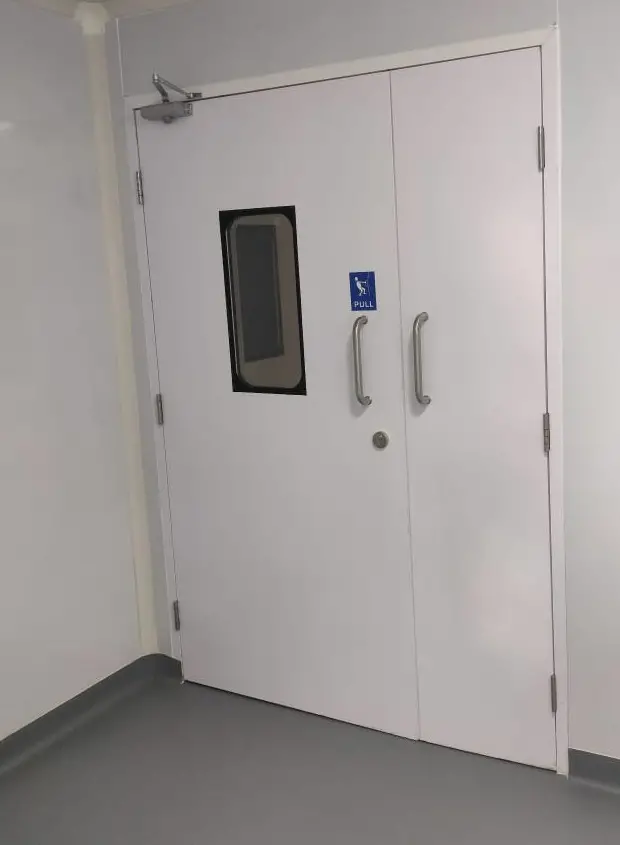
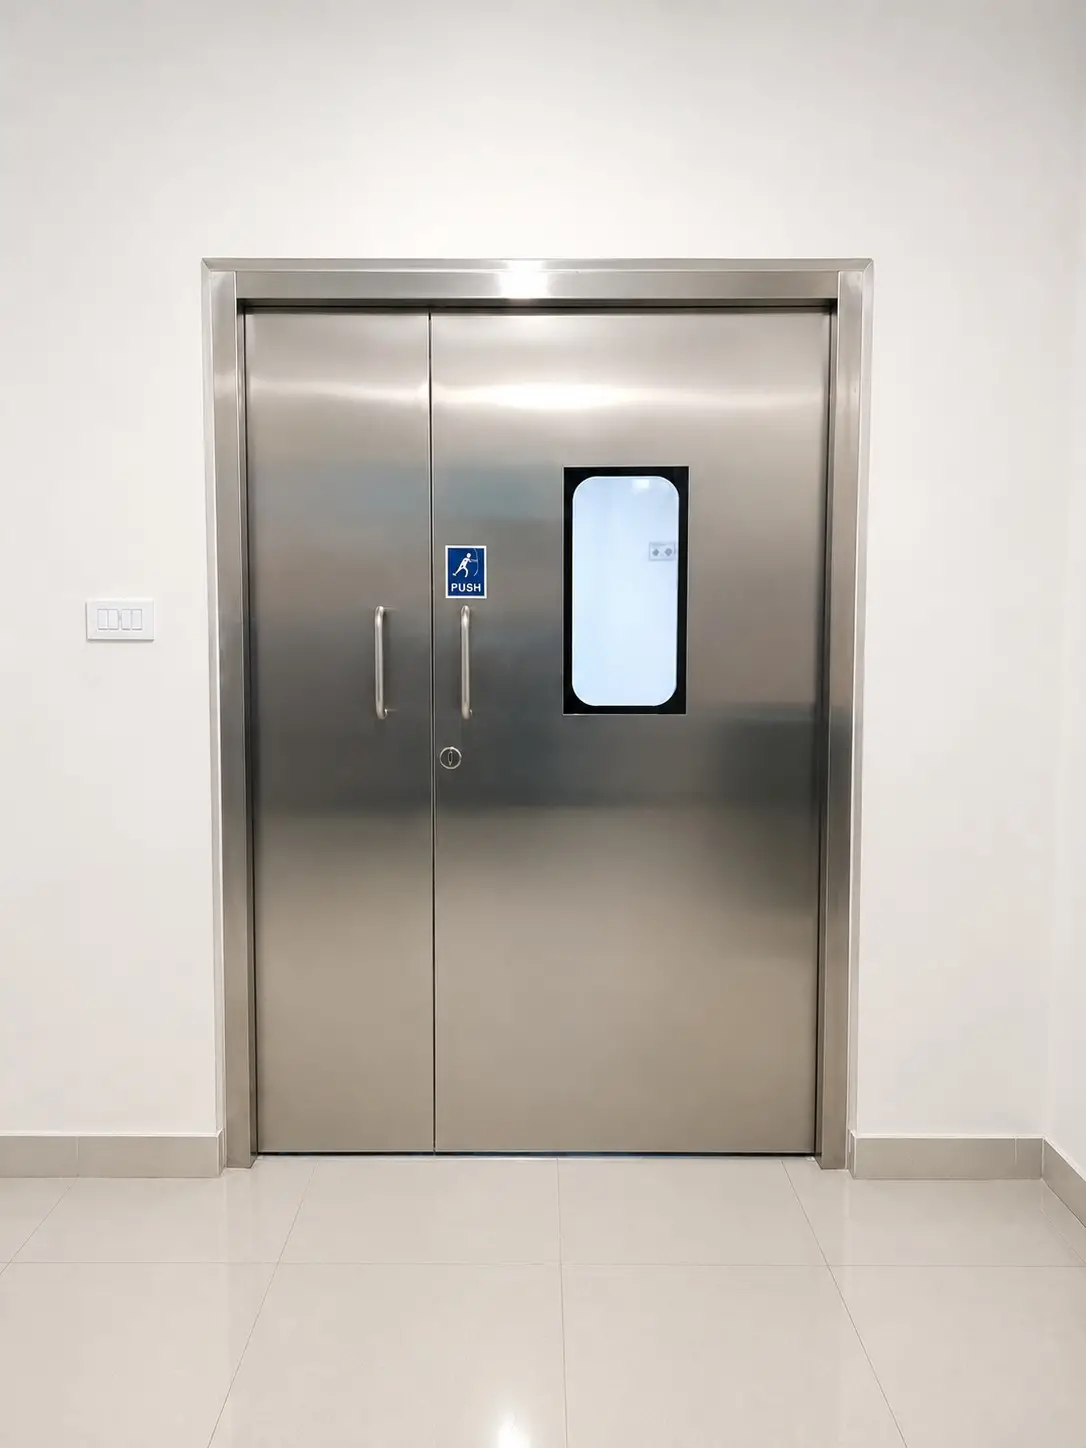
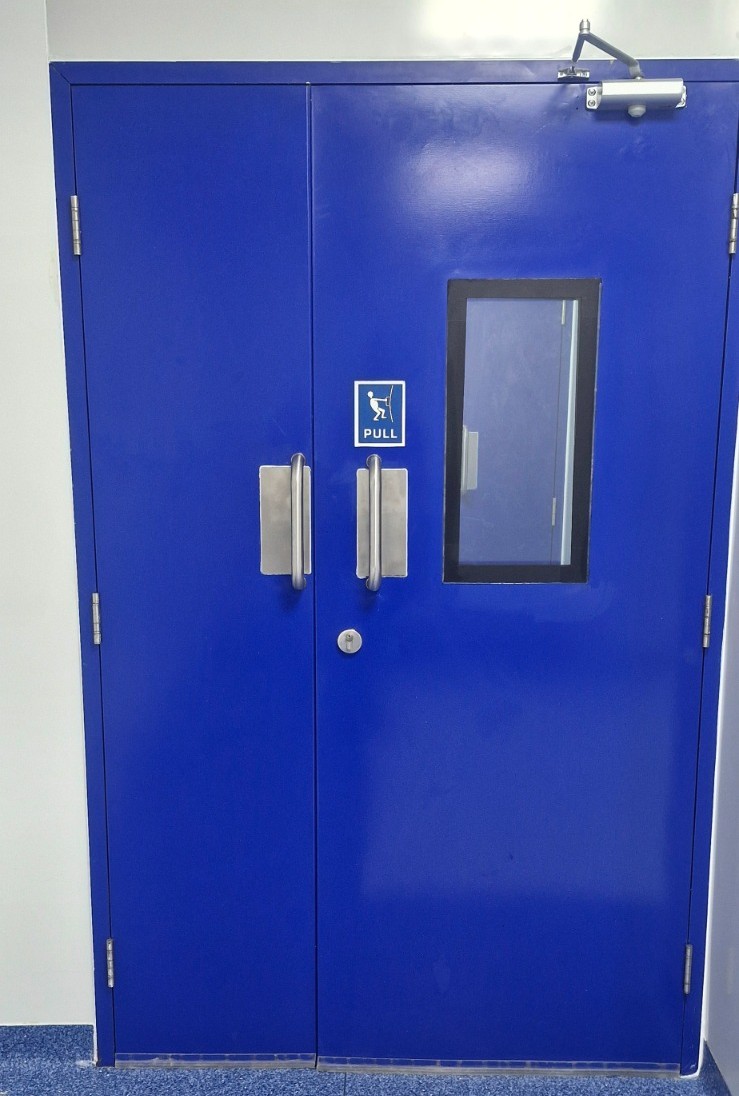
Cleanroom Door
Airtight • Hygienic • Precision-Engineered
Our Hermetically Sealed Cleanroom Doors are designed for pharmaceutical, healthcare, laboratory, and controlled environments where air leakage, contamination control, and hygiene are critical. Engineered for reliable performance, the doors provide a smooth, flush finish with durable construction and customizable configurations.
Key Features
- Airtight & Leak-Proof Design
- High-Quality Materials
- Smooth & Flush Finish
- Automatic & Manual Options
- Integrated Vision Panels
- Chemical & Moisture Resistance
Applications
Pharmaceutical Cleanrooms • Hospitals • Modular Operation Theatres • Laboratories • Biotechnology
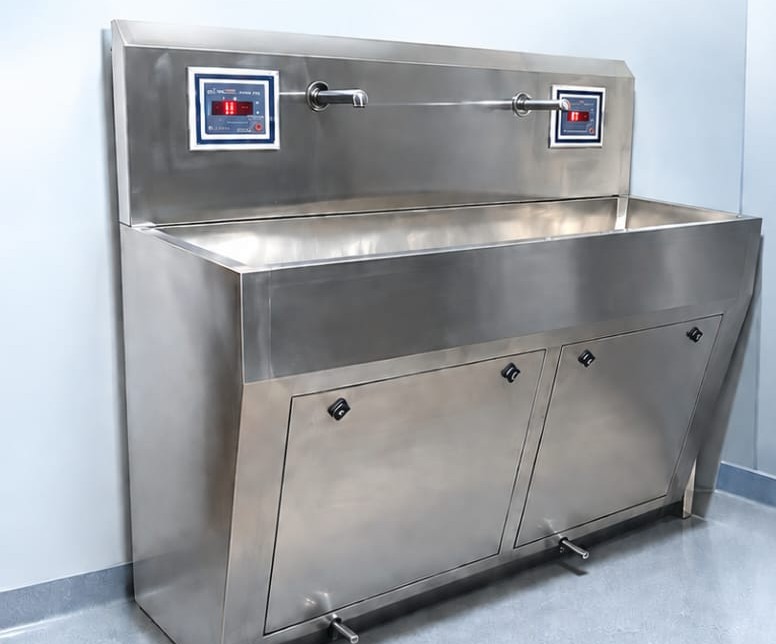
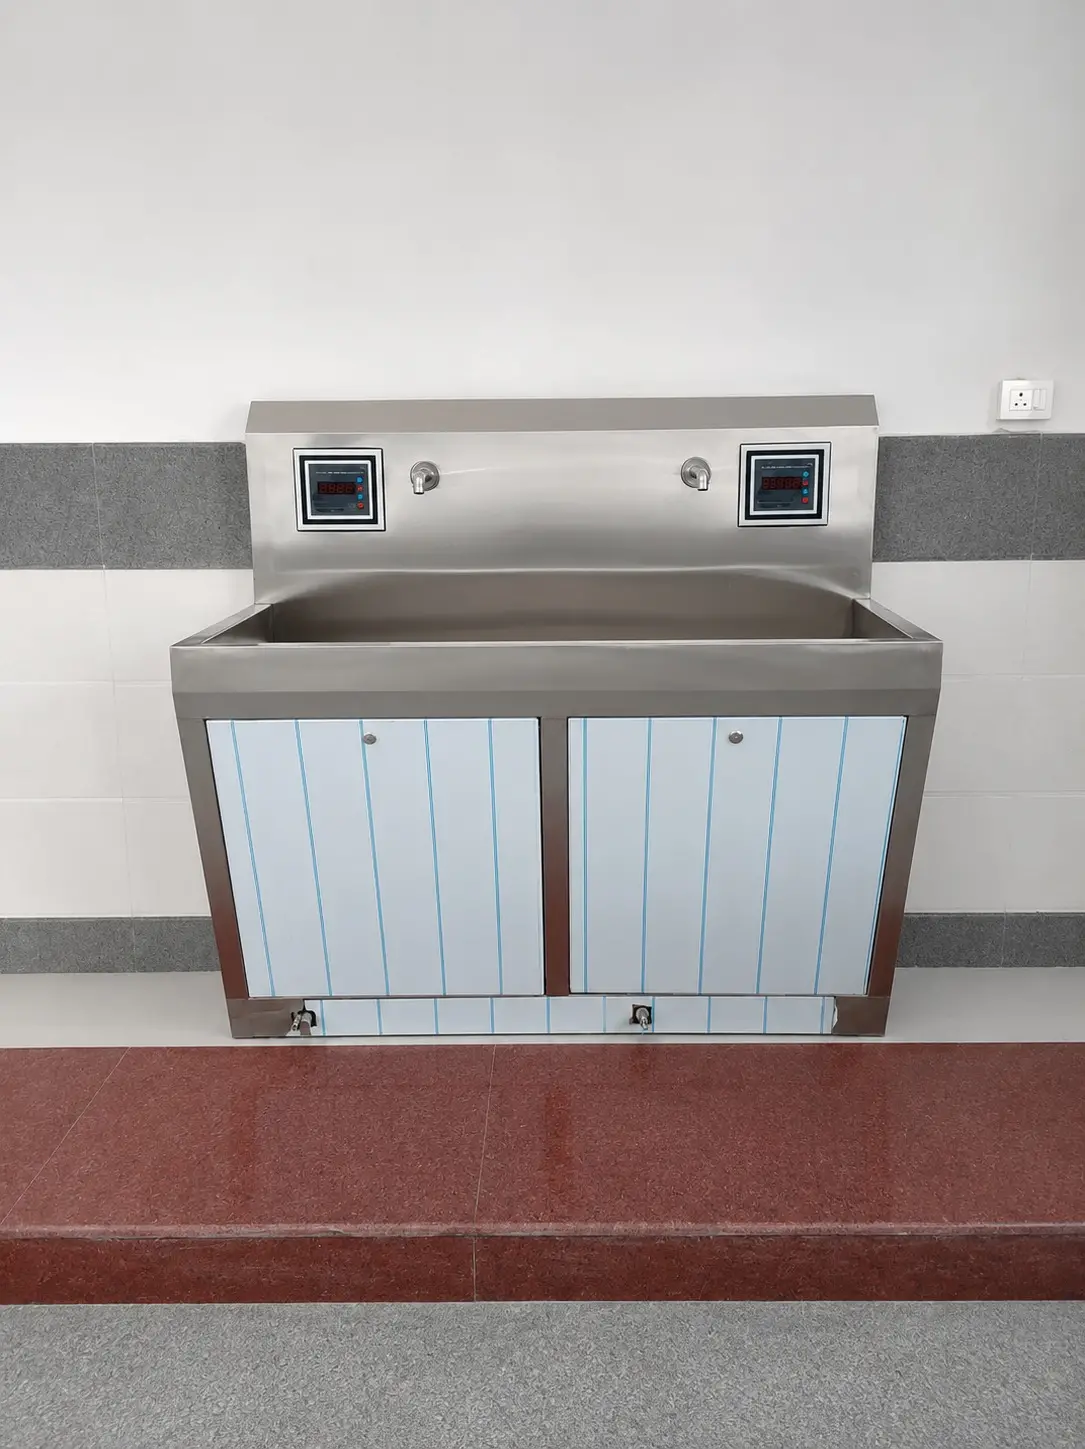
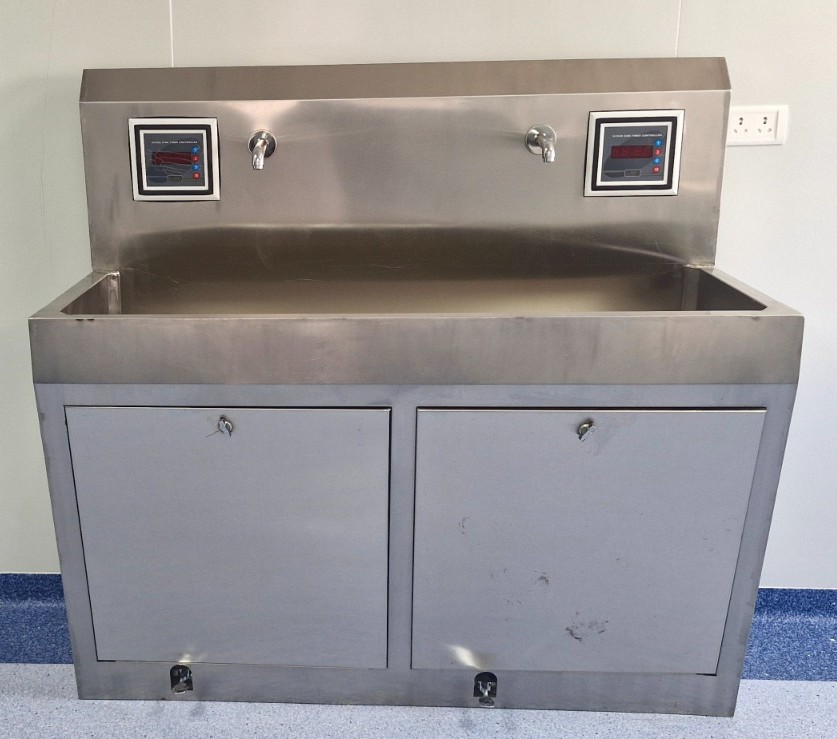
Surgical Scrub Station
Hygienic • Hands-Free • Precision-Engineered
Our Surgical Scrub Stations are engineered for operating theatres, surgical suites, hospitals, and controlled healthcare environments, providing a hygienic and efficient hand-washing solution for medical personnel. Designed with durable stainless-steel construction and practical hygiene features, they support demanding healthcare applications.
Key Features
- Hands-Free Operation
- Stainless Steel Construction
- Temperature-Controlled Water Flow .
- Integrated Soap & Disinfectant Dispensers
- Customizable Configurations
- Hygienic Easy-Clean Design
- Healthcare Application
Applications
Modular Operation Theatres | Hospitals | Surgical Suites | Medical Centres | Healthcare Facilities
OT Lights – Surgical Lighting Systems
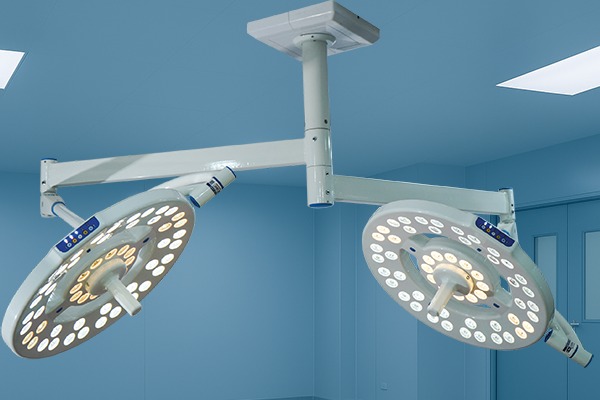
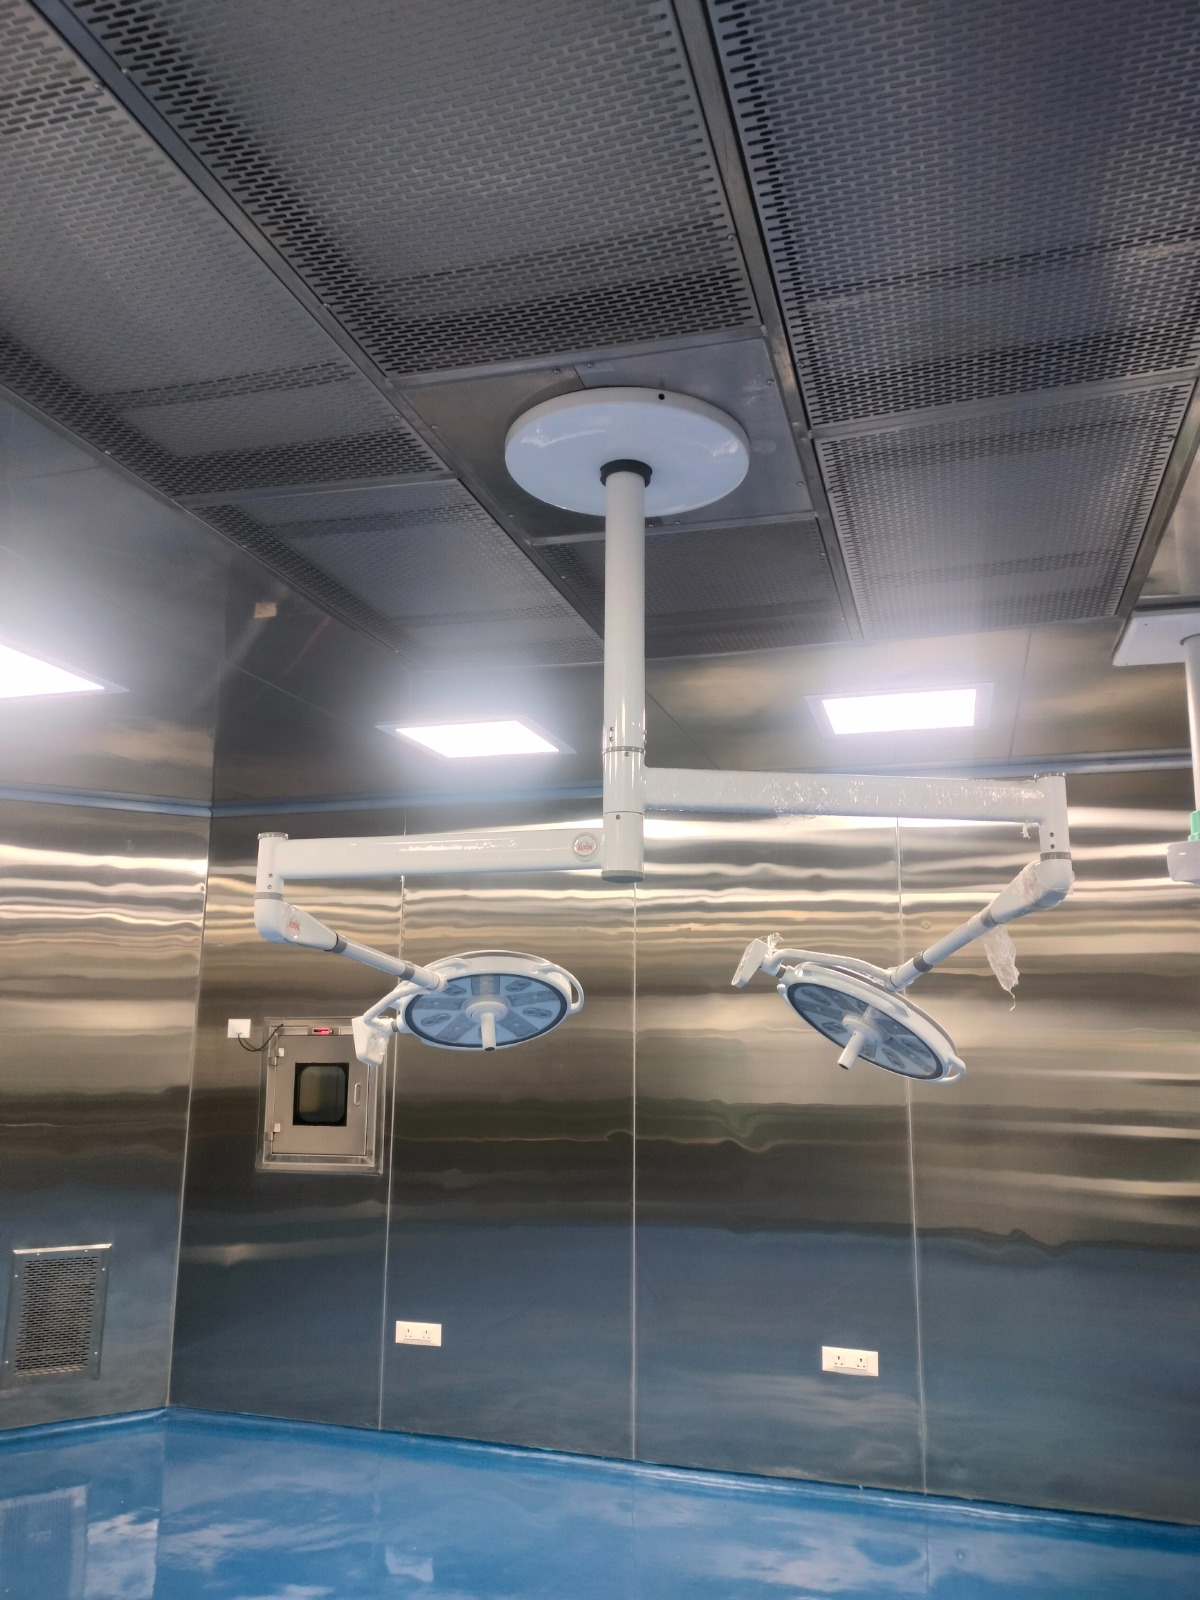
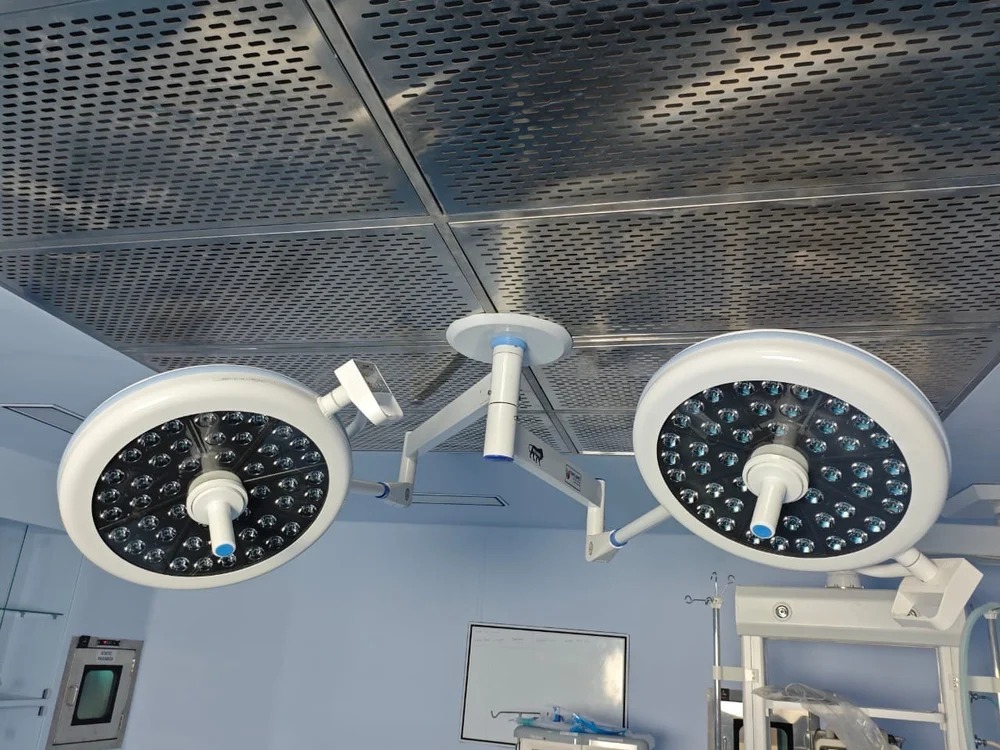
Bright • Shadow-Free • Precision-Engineered
Our OT Lights are designed to provide high-quality, shadow-free illumination for operating theatres and precision surgical procedures. Advanced LED technology delivers consistent, cool illumination with adjustable intensity and wide-area coverage for improved visibility during surgery.
Key Features
- Bright, Shadow-Free Illumination
- Adjustable Light Intensity
- Cool LED Technology
- Wide Light Coverage
- Adjustable Positioning
- Easy-to-Clean Design
Applications
Modular Operation Theatres • Hospitals • Surgical Centres • Emergency & Procedure Rooms
Medical Gas Wall Outlets
Reliable Medical Gas Access
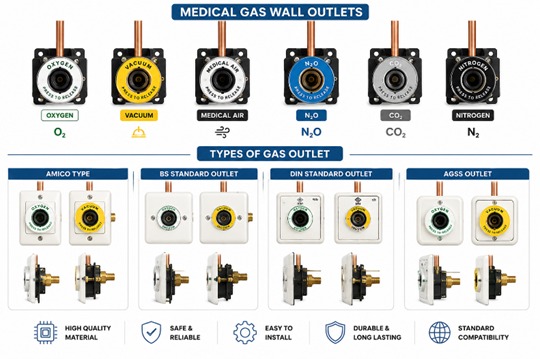
Medical gas outlets designed for integration with Medical Gas Pipeline Systems (MGPS) in hospitals and critical-care environments.
Gas Services
O₂ | Medical Air | Vacuum | N₂O | CO₂ | N₂ | AGSS
Medical Gas Outlet Types
- Amico Type Outlet
- BS Standard Outlet
- DIN Standard Outlet
- AGSS Outlet
Key Features
- Gas-specific indexing
- Clear gas identification
- Robust construction
- Easy maintenance
- Wall, bed-head & pendant integration
Applications: Hospitals | ICUs | Operation Theatres | Emergency & Critical Care
Medical Area Alarm System
Continuous Medical Gas Monitoring
Area Alarm Systems monitor medical gas pressure and provide visual and audible alerts when conditions move outside configured limits.
Key Features
- Digital pressure display
- Multi-gas monitoring
- High / low pressure alarms
- Audible & visual indicators
- Audio mute function
- Microprocessor-based control
Monitored Services: O₂ | N₂O | Medical Air | Vacuum
Applications: Hospitals | ICUs | Operation Theatres | Critical Care
Two Source Fully Automatic Gas Control Panel
Automatic Medical Gas Changeover
Automatic control panels designed to manage two medical gas sources, providing controlled source changeover for critical healthcare applications.
Key Features
- Automatic bank changeover
- Pressure monitoring
- Pressure regulation & stabilisation
- Microprocessor-based control
- Visual & audible alarms
- Source status indication
Gas Services: O₂ | N₂O | Medical Air | N₂ | CO₂
Applications: Hospitals | ICUs | Operation Theatres | Critical Care
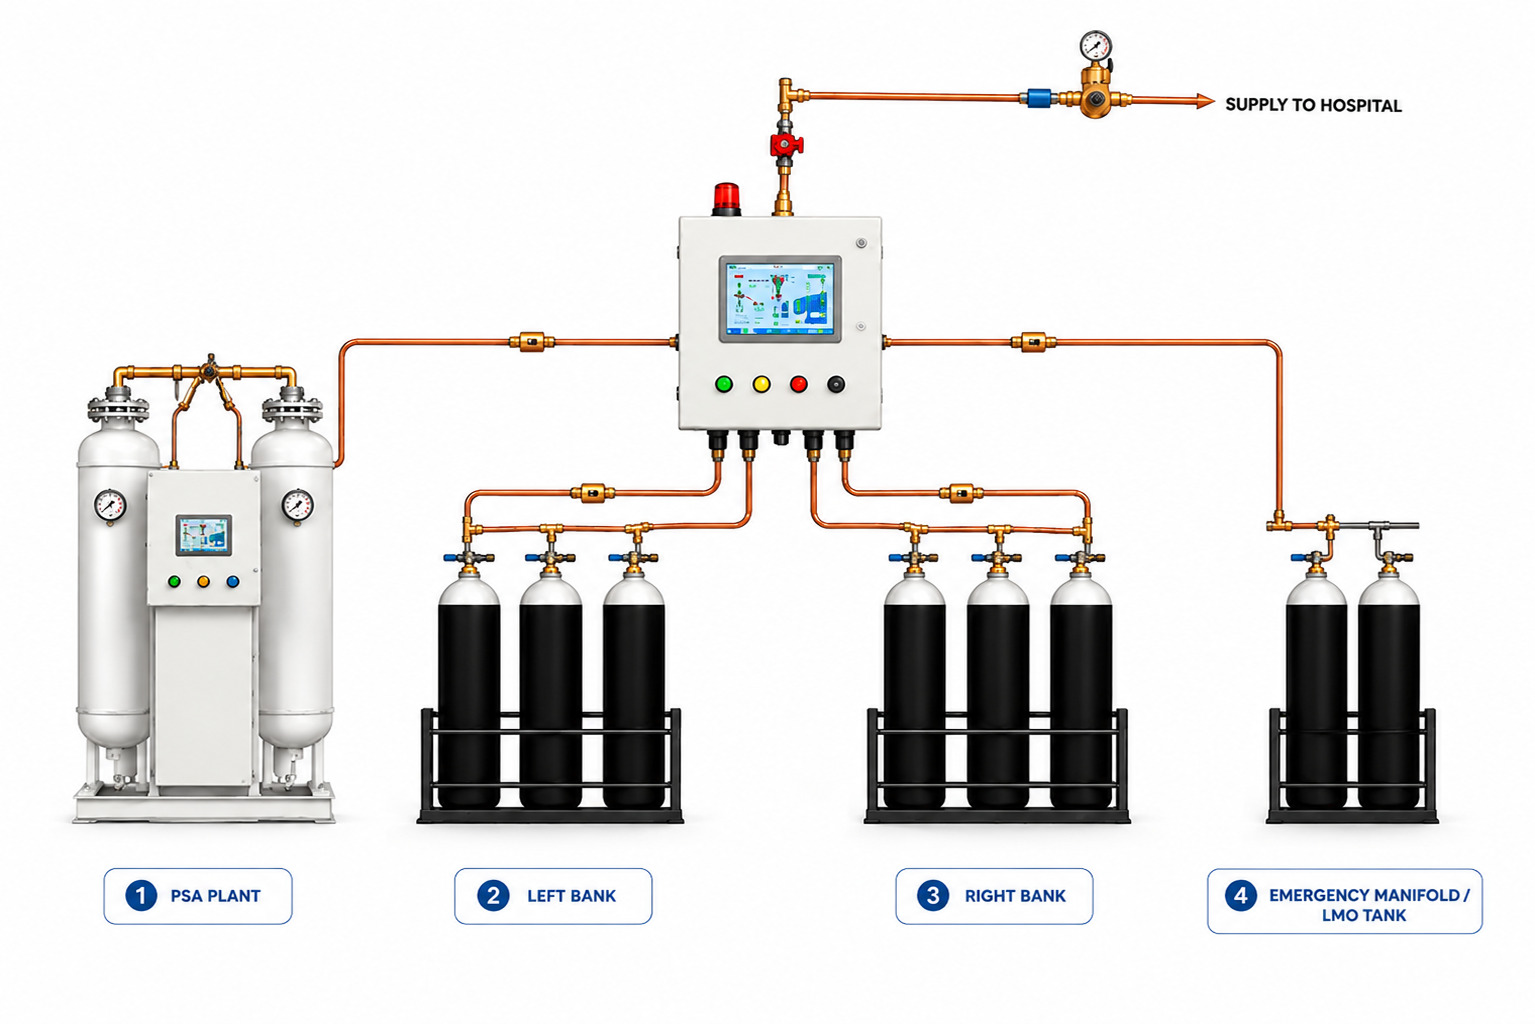
Three Source Automatic Gas Changeover
Multi-Source Medical Gas Management
Automatic changeover systems designed to manage multiple medical gas sources for reliable supply continuity in critical healthcare facilities.
Source Options
- PSA Oxygen Plant
- Left / Right Bank Manifolds
- Emergency Manifold
- LMO Tank
Key Features
- Automatic source selection
- Logic-controlled changeover
- Pressure monitoring
- High-flow configurations
- Visual & audible alarms
- Custom source configurations
Applications: Hospitals | ICUs | Operation Theatres | Emergency & Critical Care
Frequently Asked Questions
9:30 am – 6:30 PM, Mon-Sat
©Advanced Cleanroom Solutions(ACS) 2025

